Oil and gas equipment

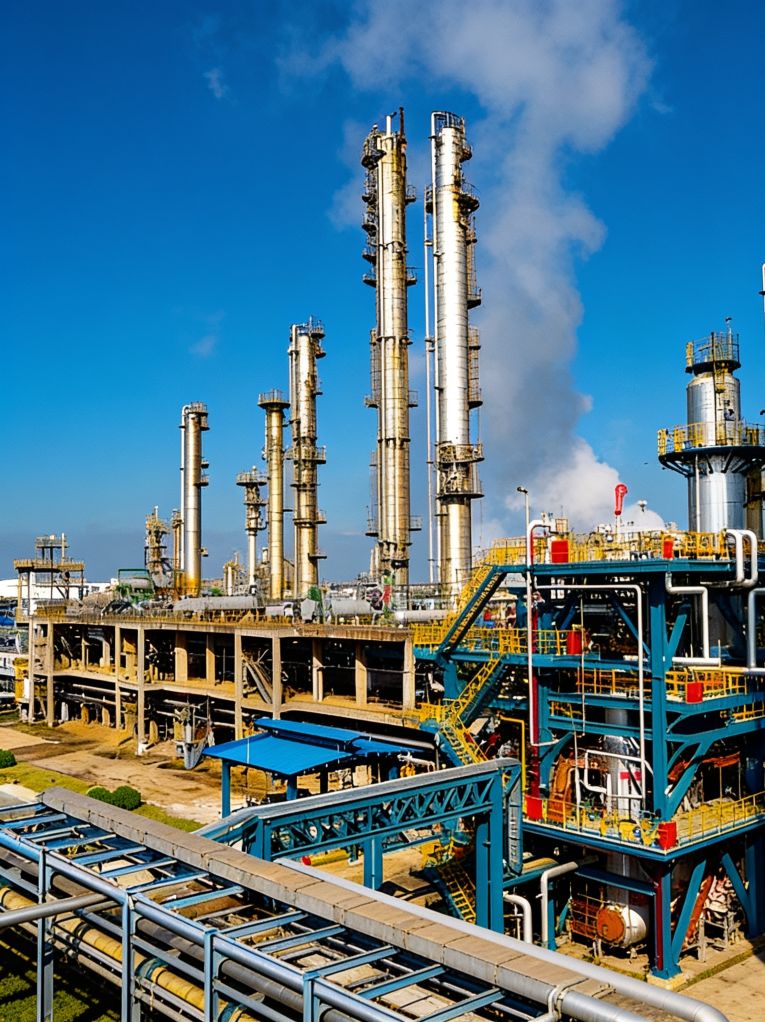
AVK provides independent selection and supply of dynamic & static equipment, valves for oil refining, petrochemical, and chemical industries, ensuring the optimal solution for each customer task.

Independent equipment selection

We act as an independent auditor, mitigating project risks during equipment procurement. AVK audits manufacturers' proposals, filters out those that fail to meet the ToR requirements, and sends them back for revision, preventing irrelevant data from reaching the customer. Our selection process is completely vendor-neutral.

50+

suppliers in the specialized equipment manufacturer database
Comprehensive approach: from process technology to mechanical design

AVK specialists' expertise in chemical and process engineering directly supports equipment selection by accounting for operating parameters and providing comprehensive project management for the order.

Financial stability of the company

AVK acts as a reliable financial partner in the transaction, which is critical given the long manufacturing lead times for equipment.

Our products

Pump units

Pump units are designed for transferring liquid process media in oil refining, petrochemical, and chemical industry processes. They ensure reliable product transportation under specified flow, pressure, and operating conditions.

Learn more
Pump units

Compressor units

Equipment for process gas compression, ensuring the maintenance of the required pressure and efficient operation of technological processes in the oil and gas industry.

Learn more
Compressor units

Pressure vessels and apparatuses

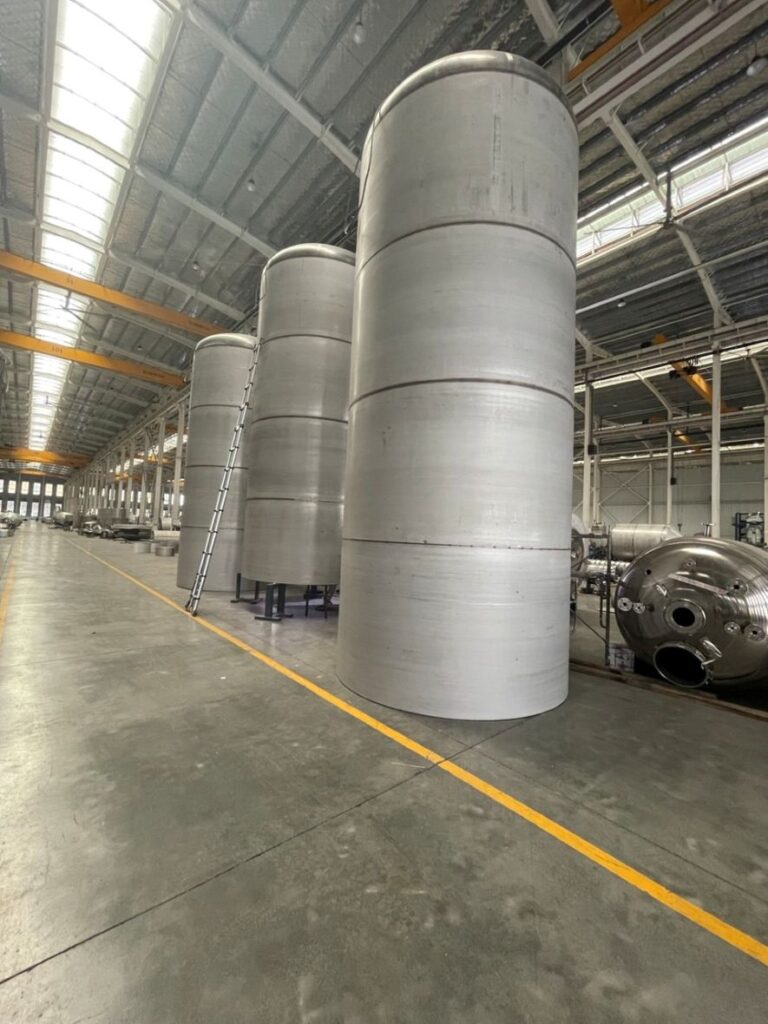
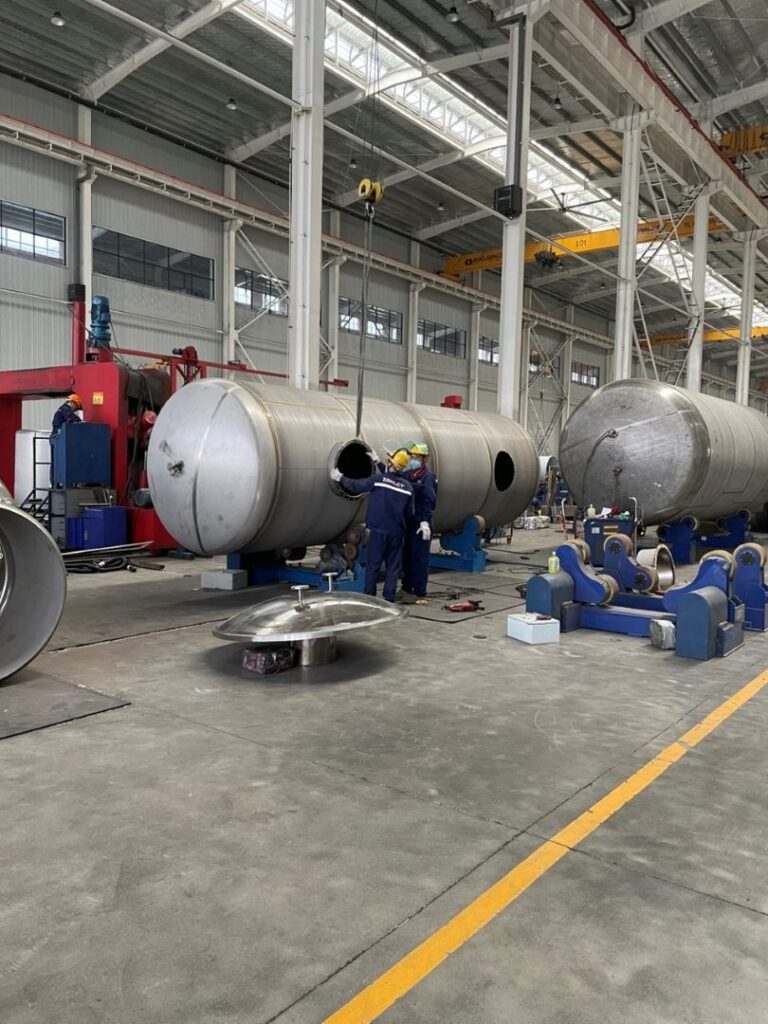
Equipment designed for operation with gas and liquid media under elevated pressure, ensuring stable technological processes in oil refining, petrochemical, and chemical industries.

Learn more
Pressure vessels and apparatuses

Heat exchange equipment

Heat exchange equipment provides heating, cooling, condensation, and vaporization of process media at oil refining, petrochemical, and chemical plants. It is selected based on process parameters, working media properties, and thermal efficiency requirements.

Learn more
Heat exchange equipment

Reactors and regenerators

Reactors and regenerators are core equipment of oil refining and petrochemical process units, ensuring reaction execution and catalyst activity restoration. Solutions are selected based on process requirements, throughput capacity, and operating conditions.

Learn more
Reactors and regenerators

Column equipment

Column equipment for the separation, purification, and processing of liquid and gas streams in oil refining, petrochemical, and chemical industry technological processes. We select all types of column equipment: fractionation columns, absorbers and adsorbers, and strippers.

Learn more
Column equipment

Column internals

Column internals are key elements of column equipment that ensure efficient heat and mass transfer in technological processes. The selection and design of mass transfer devices are performed on an individual basis, accounting for feedstock properties, throughput capacity, and the required product separation purity.

Learn more
Column internals

Process heaters / furnaces

Equipment for heating process streams in oil refining, petrochemical, and chemical industry processes, ensuring stable maintenance of specified temperature profiles.

Learn more
Process heaters / furnaces

Valves

Valves are equipment for controlling fluid, gas, and steam flows in piping systems, providing isolation, regulation, and safe operation of technological processes in the oil and gas industry.

Learn more
Valves

Filtration equipment

Filtration equipment is a critical component of process units, ensuring purification, phase separation, and system protection against particulate matter, while accounting for contaminant particle size distribution, the physicochemical properties of the filtered medium, and temperature profiles.

Learn more

Project execution

Procurement

Compliance of the technical proposal with the ToR / datasheets / specifications

Detailed design documentation

Full compliance with both the customer’s scope of requirements and the regulatory framework

Manufacturing and supply

Transparency of production and logistics stages

Supervision of installation and commissioning

We partner exclusively with contractors capable of executing the full lifecycle of service works

Operations

After-sales support

Key Advantages

Optimal selection

AVK prioritizes selecting the most optimal equipment that strictly complies with the technical specifications, fully accounting for the specific nature of the request.

Focus on the customer's objective

We are not constrained by any specific manufacturer; instead, we select the optimal equipment tailored to the customer’s objective.

Supplier audits

To mitigate risks, we conduct independent technical audits of our partners’ manufacturing facilities (including those in China) prior to order placement.

References

AVK’s core business includes the development, manufacture, and sale of industrial and specialty chemicals, as well as oil and gas equipment.
We have successfully executed supply projects for the following:

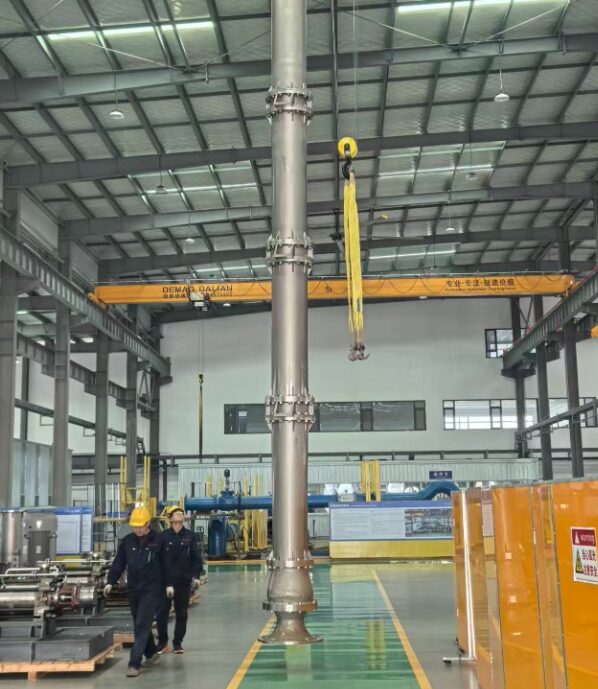
• VS4 vertical sump pumps
• Liquid ring vacuum packages
• Vessels and tanks
• Decanter centrifuges
• Automatic filters
• Column internals
• Dresser-Rand spare parts
• Sundyne pump spare parts

To review project details and our complete reference list, please leave your contact information.

Please fill out the form, and we will contact you